

Spigot elbows and tees
Moulded PE100 90° and 45° elbows and equal tees, 25–500 mm, in SDR 17, 11, 9 and 7.4 — welded pipe-to-fitting on the machine.
View detailsCombined Cooperation supplies ELOFIT PE100 butt fusion (spigot) fittings in Kuwait for welded pressure pipelines: 90° and 45° elbows and equal tees from 25 to 500 mm, reducing tees to 1000/800 mm, long and short reducers, caps, stub ends to 1000 mm with PN10 and PN16 backing flanges and gaskets, and sweep or segmented bends — each in the SDR class that matches your pipe, SDR 17 (PN10) through SDR 7.4 (PN25), with the butt welding machine sized to the largest diameter on the job.

ELOFIT spigot elbows and tees in Kuwait are moulded from 25 mm to 500 mm in SDR 11 (PN16) and from 63 mm in SDR 17 (PN10), with SDR 9 (PN20) and SDR 7.4 (PN25) patterns from 63 to 315 mm; stub ends run to 630 mm long-pattern and 1000 mm short-pattern, and reducing tees to 1000/800 mm. Pick the column that matches the pipe SDR — a PN16 fitting on SDR 17 pipe leaves a step at the weld and a PN10 fitting on SDR 11 pipe derates the line — then size the machine from the largest OD.
Moulded or fabricated depending on size, from the ELOFIT product range. PN values are PE100 on water at 20 °C.
| Fitting | SDR 17 / PN10 | SDR 11 / PN16 | SDR 9 / PN20 | SDR 7.4 / PN25 |
|---|---|---|---|---|
| Elbow 90° and 45° | 63–500 | 25–500 | 63–315 | 63–315 |
| Equal tee 90° | 63–400 | 25–400 | 63–315 | 63–315 |
| Reducing tee | 90/50 – 1000/800 | 63/32 – 630/500 | 280/63 – 500/355 | 280/63 – 450/355 |
| Cap | 63–710 | 20–630 | 63–500 | 63–450 |
| Reducer, long pattern | 75/63 – 500/400 | 32/25 – 400/355 | 63/32 – 400/355 | 63/32 – 400/355 |
| Reducer, short pattern | 200/160 – 710/630 | 200/160 – 630/560 | 200/160 – 500/450 | 200/160 – 450/400 |
| Stub end, long pattern | 63–630 | 25–630 | 63–500 | 63–450 |
| Stub end, short pattern | 110–1000 | 110–800 | 110–500 | 110–450 |
Built from pipe segments above the moulded range; see the custom HDPE fittings page for drawings.
| Type | Angles | Size range (mm) | Class |
|---|---|---|---|
| Segmented bend | 30°, 45°, 60°, 90° | 140–1000 | PE100 PN6.3 / PN10 / PN16 |
| Segmented tee | 90° | 140–1000 | PE100 PN6.3 / PN10 / PN16 |
| Segmented tee | 45° | 140–500 | PE100 PN6.3 / PN10 / PN16 |
| Sweep bend | 11°, 22°, 30°, 45°, 60°, 90° | 110–630 | SDR 17 (S8) PN10 / SDR 11 (S5) PN16 |
The stub end is fused; the flange is loose behind it and bolts to the valve or steel flange.
| Item | Range (mm) | Class / material |
|---|---|---|
| Backing flanges | 25–1000 | PN10 / PN16; aluminium, epoxy-coated steel, PP-coated cast iron, galvanized steel |
| Gaskets | 25–1000 | Standard; reinforced 50–500 |
| PE / steel plain transition, SDR 11 | 20×18 – 315×300 | Butt-weld end for steel |
| PE / steel plain transition, SDR 17 | 90×80 – 315×300 | Butt-weld end for steel |
| PE / galvanized steel plain transition | 32×25 – 315×300 | PN16 |
Fittings carry the same class as the pipe, and the class falls with temperature.
| SDR | PN at 20 °C | Allowable at 40 °C (50 yr) | Allowable at 50 °C (15 yr) |
|---|---|---|---|
| SDR 17 | 10 bar | 7.3 bar | 6.5 bar |
| SDR 13.6 | 12.5 bar | 9.1 bar | 8.2 bar |
| SDR 11 | 16 bar | 11.5 bar | 10.3 bar |
| SDR 9 | 20 bar | 14.5 bar | 13.0 bar |
From the allowable-working-pressure table in our HDPE piping catalogue (DIN 8074, safety factor 1.25). Above-ground and shallow-buried lines in Kuwait summers should be checked at 40–50 °C, not 20 °C.
Hydraulic units with heater plate, facing tool and reducing inserts.
| Machine | Pipe range (mm) |
|---|---|
| S10160 | 40–160 |
| S10200 | 63–200 |
| S10250 | 75–250 |
| S10315 | 90–315 |
| S10355 | 125–355 |
| S10500 | 200–500 |
| S10630 | 280–630 |
| S10800 | 500–800 |
| S101000 | 630–1000 |
Aligners ALL063/4 (20–63 mm), ALL225/4 (50–225 mm) and ALL315/4 (225–400 mm) for electrofusion tie-ins on the same job.
Moulded PE100 90° and 45° elbows and equal tees, 25–500 mm, in SDR 17, 11, 9 and 7.4 — welded pipe-to-fitting on the machine.
View details
Long-pattern stub ends 25–630 mm and short-pattern 110–1000 mm with PN10/PN16 aluminium, epoxy-coated or galvanized backing flanges and gaskets.
View details
Nine hydraulic sizes from 40–160 mm to 630–1000 mm with heater plates, facing tools and reducing inserts, plus hot plates and accessories.
View detailsMost butt fusion enquiries in Kuwait resolve into three either/or choices per line. This is how our team works through a fitting take-off when it arrives, and what we need from you to price it.
Potable water distribution, compressed air, plant piping and any line with surge or pumped head — the default when the schedule is silent.
Transmission mains, TSE and irrigation networks and gravity-assisted lines where 10 bar covers the duty and the thinner wall saves cost.
SDR 9 (PN20) and SDR 7.4 (PN25) patterns cover 63–315 mm for high-pressure process duties. Whatever the class, the fitting must match the pipe — check the wall table on the HDPE pipes page.
Standard 90° and 45° elbows, equal tees, reducers, caps and stub ends — stocked patterns with the full moulded wall.
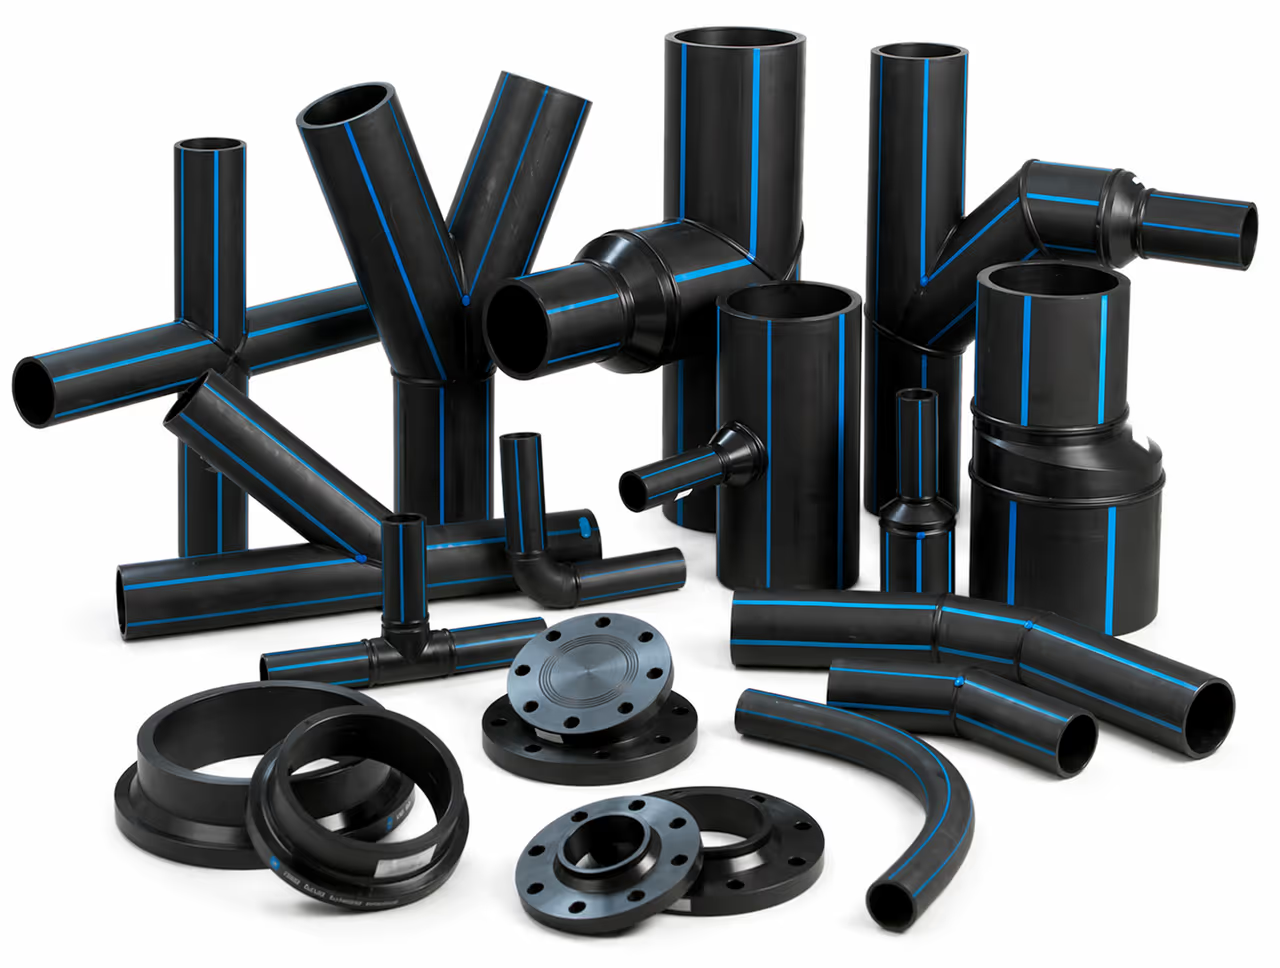
Angles other than 45° and 90°, sizes above the moulded range, reducing tees to 1000/800 mm, headers and manifolds — built to drawing, see the custom fittings page.
Segmented fittings are supplied in PN6.3, PN10 and PN16, so the operating pressure decides the pattern as much as the size does.
Valves, pumps, chambers, flow meters and steel flanges — the stub end is butt-fused, the loose flange bolts up, and the joint can be broken for maintenance.

Permanent tie-ins to steel or galvanized pipe up to 315 mm, and threaded connections to brass valves and meters below 125 mm.
Flanges come in aluminium, epoxy-coated steel, PP-coated cast iron and galvanized steel; reinforced gaskets cover 50–500 mm.

SDR 11 pipe and fittings rated 16 bar at 20 °C carry 11.5 bar at 40 °C over 50 years and 10.3 bar at 50 °C over 15 years; SDR 17 falls from 10 bar to 7.3 and 6.5 bar. Size above-ground and shallow lines at the summer temperature, not the catalogue headline.
S10160 for 40–160 mm through S101000 for 630–1000 mm. Each hydraulic unit carries the plate temperature, pressure and cooling times for every size and SDR, and reducing inserts cover the smaller pipe on the same job.
Where two fixed ends meet — at a valve chamber, a road crossing or a repair — the machine cannot pull the pipe together. Finish the run with an electrofusion coupler in the same SDR; the electrofusion fittings page lists the sizes.
Yes. We supply ELOFIT PE100 spigot fittings in Kuwait — 90° and 45° elbows, equal and reducing tees, long and short reducers, caps and stub ends — with backing flanges and gaskets, fabricated segmented and sweep bends, and the butt welding machines to join them, quoted as one package from your take-off.
Elbows and tees are moulded from 25 to 500 mm in SDR 11 (PN16), from 63 mm in SDR 17 (PN10), and from 63 to 315 mm in SDR 9 (PN20) and SDR 7.4 (PN25). Reducing tees reach 1000/800 mm, long-pattern stub ends 630 mm and short-pattern stub ends 1000 mm. Fabricated bends and tees run 140–1000 mm and sweep bends 110–630 mm.
Yes. Butt fusion melts the two walls together, so they need the same thickness for an even bead: SDR 11 fittings on SDR 11 pipe, SDR 17 on SDR 17. A thicker fitting on thinner pipe leaves a step at the joint, and a thinner fitting on thicker pipe derates the whole line to the fitting's class.
With a butt-fused stub end and a loose backing flange — aluminium, epoxy-coated steel, PP-coated cast iron or galvanized steel in PN10 or PN16, 25–1000 mm — bolted to the valve or steel flange with a gasket. For permanent tie-ins to steel up to 315 mm, a PE-to-steel plain transition welds to the PE on one side and to the steel on the other.
It falls with temperature. From our HDPE catalogue, SDR 11 rated 16 bar at 20 °C carries 11.5 bar at 40 °C over 50 years and 10.3 bar at 50 °C over 15 years; SDR 17 drops from 10 bar to 7.3 and 6.5 bar. Check above-ground and shallow-buried lines against the summer temperature, and buried mains against the soil temperature.
One that covers the largest pipe on the job: S10160 for 40–160 mm, S10200 for 63–200, S10250 for 75–250, S10315 for 90–315, S10355 for 125–355, S10500 for 200–500, S10630 for 280–630, S10800 for 500–800 and S101000 for 630–1000 mm. Reducing inserts take the smaller sizes on the same machine.
For the joints the machine cannot make: tie-ins between two fixed ends, repairs, service connections off a live main, constrained trenches, and fittings below 315 mm where a coupler is faster. Long straight runs from 110 mm and moulded spigot fittings on larger mains stay with butt fusion.
Yes. Send the pipe OD and SDR for each line, the fitting list with quantities, the flange class and material for stub ends, the medium and operating temperature, whether a machine is needed, and the delivery area in Kuwait, and we return a line-priced offer with ELOFIT codes within 24–48 hours.
Share the BOQ, drawing, pipe size, pressure class, or product list and our team will respond with a coordinated offer.
